A bad welding hire costs far more than the hourly rate once rework, reinspection, foreman time, and schedule recovery add up. This article breaks down those costs and how to screen and test welders against the work before they reach the floor.
A bad welding hire costs far more than the hourly rate. Rework pulls your best welder off scheduled work, eats up foreman time, adds another round of inspection, and forces the shop to recover the schedule with overtime. Once that pattern starts, the cheaper hire can become the most expensive person on the floor.
Not every failed weld comes back to the welder, so check the fit-up, prep, consumables, equipment, and WPS first. If those pieces are right and the same person keeps producing bad joints, missing obvious problems, or needing constant supervision, you have a hiring problem.
The cost shows up across production, quality, and delivery, which is why the screening needs to match the work before anyone reaches the floor.
1. Your best welders become the repair crew
When a weld fails visual inspection, UT, or RT, the repair usually goes to somebody you trust. You are not handing critical code work back to the same person and hoping the second try works.
Now your best fitter-welder, lead hand, or structural welder is grinding out somebody else’s work instead of moving their own job forward. The shop pays for the repair, and it also loses the production that an experienced welder was supposed to deliver.
The cost includes:
-
Cutting, gouging, and grinding out the failed weld
-
New consumables and joint preparation
-
Repair labor at your stronger welder’s rate
-
Reinspection
-
Lost output from the job they stepped away from
Payroll shows a full shift, but the floor loses ground. The assembly stays in the bay, paint gets pushed, and the next crew inherits unfinished work.
The foreman gets pulled in too. Every new welder needs time to learn your prints, procedures, equipment, and quality expectations, but constant checking turns onboarding into another responsibility.
If every root pass needs approval, every setup needs correction, or every questionable joint gets caught by somebody else, your foreman is babysitting one hire instead of running production.
One person like that can slow a crew, while two or three can make a fully staffed shop feel short-handed.
2. Rework eats the schedule faster than the budget shows
Most shops see the repair hours, while fewer track everything tied to them.
Once a weld fails, the part stops moving. Somebody writes the NCR, the joint gets evaluated, the repair is planned, the defect is removed, and the weld goes back through inspection. If your CWI or outside inspector cannot get there until the next day, the assembly sits while the schedule keeps moving around it.
The direct cost is easy to see:
Removal + prep + repair labor + consumables + reinspection
The full cost is wider:
Direct repair cost + lost production + overtime + schedule recovery + freight or delivery penalties
A repair can climb quickly once you include your lead welder’s lost hours, the foreman’s time, another inspection window, and the overtime needed to recover the date.
Then estimating starts missing the floor.
Most shops build some allowance for scrap and rework into the bid, which only works when the number reflects the floor. If repair hours have climbed over the last six months and estimating still uses last year’s rate, every new job starts with the wrong assumption.
You win the work using an old number, then produce it with a more expensive crew.
Customer trust gets pulled into it too. One internal repair may never leave the building, but a pattern eventually shows up through late deliveries, rejected assemblies, and extra documentation.
Code work leaves far less room for vague credentials. AWS D1.1 structural welding, ASME Section IX, and API 1104 each carry different requirements. A resume that says “certified welder” alone tells you very little unless the process, position, material, thickness range, and continuity line up with the job.
3. A “qualification card” does not tell you how someone works
A welder can hold a qualification and still be wrong for your floor.
A shop running FCAW on structural steel needs a different background from a manufacturer doing GTAW on stainless pipe. Somebody who spent three years on repetitive GMAW production may be solid in that setting and struggle with one-off structural fit-up, and the reverse can happen too.
“Five years of welding experience” alone hides the useful details.
Before you move a candidate forward, check:
-
The processes they have run: SMAW, GMAW, FCAW, or GTAW
-
The positions they have welded in
-
The materials and thicknesses they have worked with
-
Their experience with AWS D1.1, ASME Section IX, API 1104, or another code
-
Whether the qualification is current and continuity has been maintained
-
Whether their last shop handled repetitive production, structural fabrication, pipe, pressure work, or custom builds
Then test the actual work.
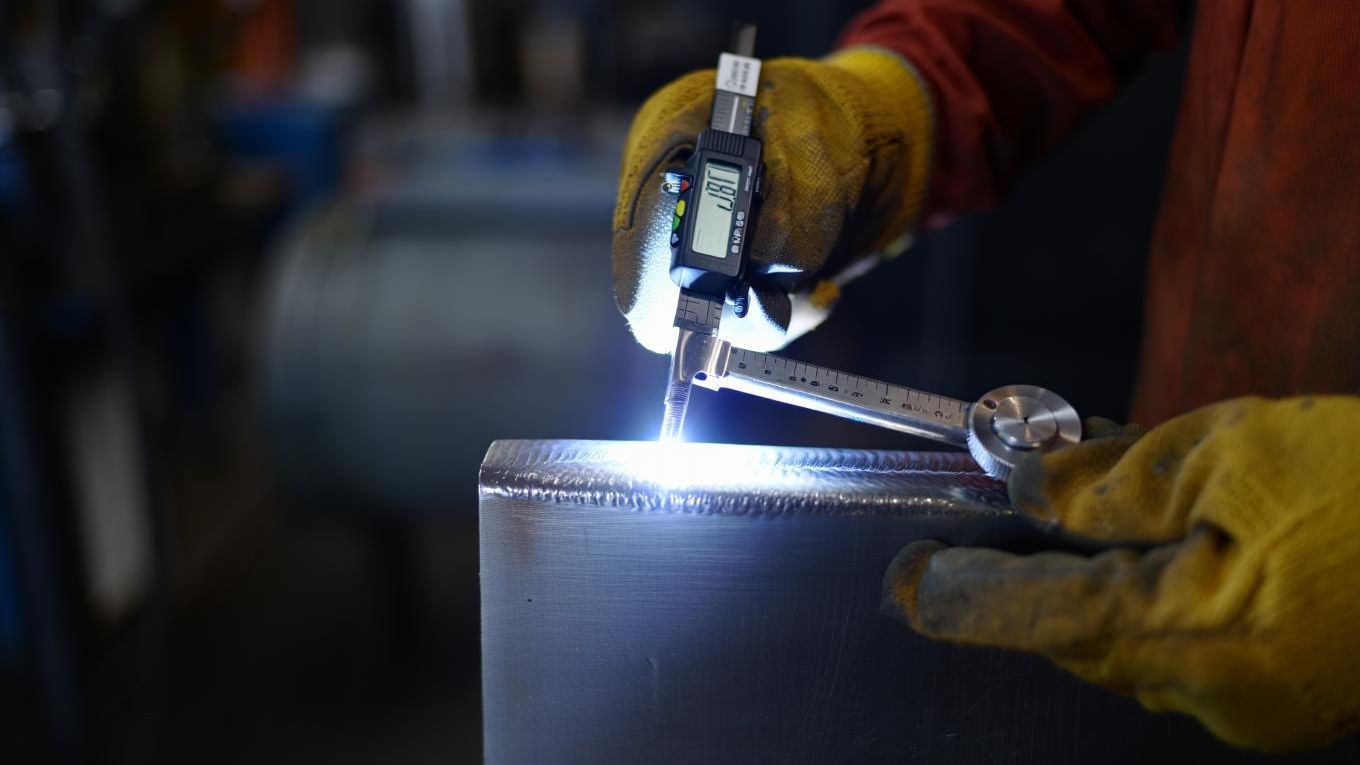
A flat plate coupon tells you little when the job requires out-of-position structural work, thick plate, tight access, or real fit-up. Match the test to the process and position they will run, and have somebody knowledgeable watch the setup.
The finished coupon matters, but the setup shows how the person thinks. Watch whether they:
-
Check fit-up before starting
-
Confirm machine settings and consumables
-
Follow the WPS
-
Handle starts, stops, and restarts cleanly
-
Speak up when something falls outside tolerance
-
Know when a joint can be corrected and when it needs to go back
A good welder does not burn through bad fit-ups and hope inspection accepts it. They stop, raise the issue, and protect the job before the defect gets buried under another pass.
The same logic applies to fitter-welders. A person may lay down a good bead and still struggle to read prints, lay out parts, or work through fit-up. If the job requires fitting and welding, test both.
4. Weak recruiting pushes the screening back onto your shop
Most bad placements start before the candidate reaches the floor.
You ask for a structural fitter-welder, and a recruiter sends somebody who spent two years doing spot welds on an assembly line. You ask for a CNC machinist with Fanuc controls, and they send someone whose entire background is basic machine operation. The resume contains the right keywords, so the recruiter submits it and leaves your foreman to sort it out. That’s what you call resume forwarding dressed up as recruiting.
A recruiter working in steel and metal trades should confirm:
-
The process, code, position, and material the shop runs
-
Whether the role requires fitting, welding, or both
-
The prints the person will need to read
-
The machines, controls, and tooling on the floor
-
The test the candidate will need to pass
-
The details the recruiter verified rather than accepted at face value
They should understand why Fanuc and Siemens experience differ, why a Haas operator may need support before stepping onto a Mazak, and why AWS D1.1 structural experience gives you no automatic proof of ASME Section IX capability. Technical fluency saves your team time. Without it, your shop becomes the recruiter’s screening department.
5. Contract-to-hire gives you time to verify the full picture
A weld test can show whether somebody performs under test conditions, while four months on the floor reveal attendance, pace, consistency, teamwork, response to feedback, and quality across different jobs.
Cannonball uses contract-to-hire for 99% of its placements.
The shop sees the person on its equipment, under its procedures, with its prints and quality standards. The welder sees the schedule, supervision, overtime, and work they were promised.
After four months, 87% of our contract-to-hire placements convert.
That conversion rate comes from doing the work before the start date and staying involved after it. We check performance, attendance, quality, and fit after the contractor walks through the door.
Your team controls the final qualification for the work, and contract-to-hire gives you a cleaner way to evaluate the full picture before making the long-term call.
The best time to catch a bad welding hire is before production. Get clear on the process, code, material, and shop experience you need, use a weld test that matches the work, and check how the person sets up, responds to problems, and handles the pace of the floor. Contract-to-hire gives you time to confirm the fit before making the long-term call.
A cheap hire stops being cheap the minute your best welder has to repair their work.
Cannonball Recruiting works with steel fabricators, machine shops, and metal manufacturers that are tired of agencies sending warm bodies and calling them tradespeople. We screen for the work you run, speak the language your foreman speaks, and stay involved while the person proves they belong on the floor.
When rework starts climbing, look at the process first. If the process is sound and the same person keeps producing the failures, stop paying your best people to cover for the wrong hire.
Frequently Asked Questions
What does a bad welding hire actually cost a fab shop?
Beyond the repair itself, your best welder gets pulled off scheduled work, the foreman spends time supervising, the weld goes back through inspection, and overtime goes into recovering the schedule. Freight or delivery penalties and lost customer trust can follow.
How do I know if failed welds are a hiring problem?
Check fit-up, prep, consumables, equipment, and the WPS first. If those are right and the same person keeps producing bad joints, missing obvious problems, or needing constant supervision, you have a hiring problem.
How should I test a welder before hiring?
Match the test to the process and position they'll run, and have someone knowledgeable watch the setup. Look at whether they check fit-up, confirm settings and consumables, follow the WPS, handle restarts cleanly, and speak up when something falls outside tolerance.